Hey there, let’s talk about something that’s probably not top of mind when you first glance at a softgel machine—temperature control. I’m not here to bore you with jargon that makes you reach for the coffee pot, either. If you’ve ever worked with softgels, you know that one tiny temp blip can turn a perfect batch into a mess of sticky, misshapen capsules that go straight to the trash. As someone who’s been selling and tweaking softgel machines for over a decade, I’ve seen more projects derailed by bad temp control than by any other single factor. So let’s break this down like we’re chatting over a workshop bench, no fancy textbooks required. Softgel Machine
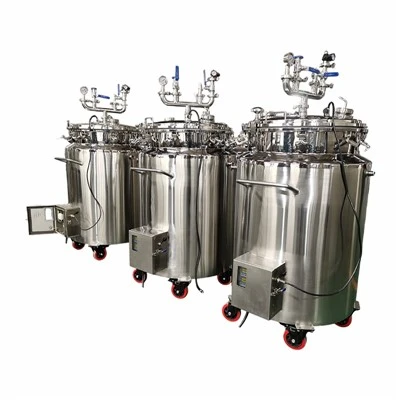
First off, let’s get one thing straight: softgels aren’t just pills in a fancy shell. They’re a two-part system—the gelatin shell and the liquid (or semi-solid) fill inside—and both have very specific moods. Gelatin, the main ingredient in the outer shell, is a protein derived from collagen, usually from animal bones or skin. It’s finicky: melt it too hot, and it breaks down, becomes brittle, or loses its ability to set properly. Cool it too fast, and it doesn’t flow right through the die plate (the part that shapes the capsules) so you get lopsided, incomplete ones. Then there’s the fill—whether it’s a fish oil supplement, a CBD oil blend, or a vitamin paste. That stuff has its own temp sweet spot too. Too warm, and it might thin out, leak through the shell, or even oxidize faster. Too cold, and it gets too thick to pump accurately, leading to inconsistent fill volumes. Temperature control isn’t just a “nice-to-have” on a softgel machine—it’s the backbone of making softgels that are safe, uniform, and shelf-stable.
Now, let’s talk about where temperature control actually lives on a softgel machine, because it’s not just one switch in a control panel. Most modern softgel machines are set up in zones, and you’ve got to nail each one. The first zone is the gelatin hopper and conditioning system. That’s where the gelatin mix (gelatin, water, plasticizers like glycerin, and sometimes colorants or flavors) is melted and prepped into a smooth, workable liquid. I’ve seen cheap machines that just blast heat from a single element, which causes hot spots in the hopper—parts of the gelatin mix are 10°F hotter than others, leading to uneven shell viscosity. A good machine (the ones I sell, anyway) has jacketed hoppers with circulating temperature-controlled fluid, so the heat is uniform across the entire mix. We’re usually targeting 120–140°F here, right around the point where gelatin is liquid but not breaking down. If you go over 150°F, gelatin starts to hydrolyze—think of it like cooking a hot dog too long; it gets rubbery and loses its stretch. That’s the last thing you want when you’re running the die rollers, which press the gelatin sheets into capsules.
Speaking of die rollers, that’s the next critical temp zone. The two die rollers are what actually stamp the capsule shape, cut it, and seal the edges. They have to be just the right temperature so the gelatin sticks together when pressed, but not so cold that the sheet gets rigid and cracks. This is where a lot of new operators mess up—they see a sticky sheet and crank the rollers colder, but that makes the seal weak. Or if the sheet is tearing, they crank the rollers warmer, and the seal leaks. I always tell customers to test with a small batch first: run a 10-minute trial, check the seal strength (you can gently pull two sealed capsules apart—if they split clean, no leak, that’s good), and adjust the roller temp by 2–3°F at a time. Typical roller temps are around 70–90°F, depending on the gelatin formula and room humidity. Oh, and humidity is tied to this, by the way—if your facility is super dry, you might need slightly warmer rollers to keep the gelatin from drying out too fast mid-stamp. It’s a dance, not a set-it-and-forget-it thing.
Then there’s the fill system, which is often overlooked. The liquid inside the capsules—whether it’s oil, paste, or something else—needs to be at a consistent temp so its viscosity stays the same. If the fill is too thick, the pump can’t push enough into each capsule, leading to under-filled units. Too thin, and you get over-filled, or even spillage when you seal. For most oil-based fills, we keep the fill chamber at 85–100°F, which thins the oil just enough for accurate pumping without making it runny. For thicker pastes, it might be a bit higher, but we never go above 110°F because some active ingredients (like certain vitamins or herbal extracts) degrade with heat. Good machines have inline temperature sensors on the fill line, so if the temp drifts even 1°F, the system adjusts automatically. Cheaper machines just have a dial that you set once, and if the room temp changes (like if your AC kicks on in the middle of a run), the fill temp goes off and you get a bad batch.
Wait, let’s not forget the drying and curing zone, either. Once the capsules are formed, they go into a tumble dryer or a curing chamber to remove excess moisture. This is where you finish setting the gelatin shell, so it’s hard enough to handle and doesn’t stick together. If the dryer is too hot, the outside of the capsule dries too fast, trapping moisture inside—those will get moldy before they even hit the shelf. Too cool, and they stay soft, stick to each other, and ruin the entire batch. Most curing zones run at 95–110°F with low airflow, and it takes 12–24 hours, depending on the capsule size. I always advise customers to use a humidity gauge here too—if the room is humid, you might need to lower the dryer temp just a little, because moisture won’t evaporate as fast.
Now, why does this matter for you, the operator or the manufacturer? Let’s do the math. If you have a 10,000-capsule batch, and your temp control is off just 5°F in the die rollers, you might get 15–20% of the capsules with weak seals. That’s 1,500–2,000 capsules wasted. Multiply that by 10 batches a week, and you’re throwing away thousands of dollars every month. Not to mention, inconsistent temp control can lead to compliance issues—if you’re making supplements or pharmaceuticals, regulators want every capsule to be uniform, from fill volume to shell quality. A bad batch can mean a recall, which is way more expensive than the cost of a reliable machine with good temp control.
Here’s the thing I always tell new customers: not all softgel machines’ temperature control is created equal. Some cheap import machines use basic heating elements and no feedback sensors—they just turn on when the temp drops and off when it spikes, leading to swings of 10°F or more. My team designs our machines with closed-loop temperature controllers, which constantly monitor the actual temp and adjust the heat or cooling in real time, keeping swings to less than 2°F. We also have separate zones for every part of the process, so you can tweak the gelatin hopper without messing with the die rollers or fill system. That level of precision isn’t just a luxury—it’s how you make quality softgels consistently, run longer batches without stopping to fix messes, and keep your costs down.
I also want to mention common mistakes I see operators make when dealing with temp control. First, ignoring the room environment. If your production floor is too cold (below 65°F) or too hot (above 85°F), it throws every zone off. We always recommend a dedicated production room with temperature and humidity control, or at least make sure the softgel machine isn’t placed near a door, window, or AC vent that causes drafty spots. Second, not calibrating the temp sensors regularly. Those little sensors on the machine can get coated with gelatin or fill residue over time, so they read wrong. We tell customers to check and calibrate the sensors once a month, or every 50 operating hours—something that takes 10 minutes but makes a huge difference. Third, cranking the heat to fix problems instead of troubleshooting. If your capsules are leaking, don’t just turn up the die roller temp—check the gelatin mix first, check the seal pressure, check the fill temp. Temp is part of the puzzle, not the only solution.
Let’s wrap this up with a quick example. A couple years back, we had a customer who was getting 20% scrap on their CBD softgel batches. They were using a machine they’d bought cheap online, and the temp control was all in one panel—they’d set the total machine temp to 100°F, and that was it. The gelatin hopper was actually at 140°F (too hot, breaking down gelatin), the die rollers were at 55°F (too cold, cracking seals), and the fill was at 105°F (too hot, making CBD oxidize). We swapped them to one of our machines with zone-specific temp control, calibrated their sensors, and within a week their scrap was down to 2%. They saved over $20,000 a quarter just by fixing their temp control game. That’s not an exaggeration—that’s real stuff, from real small manufacturers who came to me frustrated after wasting money on bad equipment.
At the end of the day, temperature control on a softgel machine isn’t about having the fanciest tech—it’s about consistency. You need every capsule to be identical, from the first one rolled to the last one, so your customers trust your product, and you don’t waste time or money fixing avoidable issues. If you’re in the market for a softgel machine, don’t just ask about capacity or price—ask about temperature control: how many zones does it have? What kind of controllers are used? How do you adjust for different formulas or room conditions? If a supplier can’t answer those questions clearly, that’s a red flag.
If you’re tired of dealing with bad batches, high scrap rates, or machines that can’t keep up with your production needs, we can help. We’ve spent years refining our softgel machines’ temperature systems to be reliable, precise, and easy to adjust, no matter what kind of softgels you make—whether it’s fish oil, vitamins, supplements, or pharma-grade capsules. We work with small startups and large manufacturers alike, so whatever your volume or formula needs, we can walk you through the best setup. Reach out to us to talk through your specific needs, and we’ll help you stop fighting temperature issues and start making great softgels.
Bottle Filling Machine References:
- Gibson, J. Softgel Technology: Principles and Practice. Pharmaceutical Press, 2018.
- Parenteral Drug Association. Temperature Control in Pharmaceutical Manufacturing: Best Practices. PDA Book Series, 2021.
- Zhang, L. “Effect of Temperature on Gelatin Viscosity and Softgel Seal Integrity.” Journal of Pharmaceutical Sciences, vol. 109, no. 4, 2020, pp. 1456–1462.
Wenzhou Vitol Machinery Co., Ltd.
As one of the most professional softgel machine manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy customized softgel machine made in China here from our factory. Also, quotation is available.
Address: #16 Yongen Road, Longwan Area, WenZhou, Zhejiang, China
E-mail: leapeng01@gmail.com
WebSite: https://www.vitolsoftgel.com/
